Damaging Pump Cavitation: Non-intrusive Measurement Method
Summary
What threshold vibration acceleration measurement value confirms that cavitation is likely causing metal removal damage? Mechanical Solutions (MSI) utilizes an innovative high-frequency accelerometer technique for quantifying the amount of metal damage when cavitation-like noise is observed. The method is applicable to pumps, valves, and other fluid system components. MSI can estimate the severity of the metal removal damage, if any, to determine if component modifications are essential (for meeting reliability) or determine that the cavitation noise is simply a nuisance.
In this specific case, the high-frequency accelerometer measurements identified acceleration levels up to four times the level associated with damaging cavitation. The investigation identified cavitation surge (Figure 1) and suction recirculation (Figure 2) as key contributors.
An impeller re-design and material modifications increased expected impeller life from less than two years to approximately 15 years and generated approximately $840,000 in repair-cost savings across four pumps.
What was the pump problem?
The pumps produced a periodic "chugging" sound while operating at approximately 100% to 130% of best efficiency point (BEP). Operation in this flow range was required to meet the system's operating profile.
The owner needed to determine without pump disassembly for inspection whether the noise was harmless cavitation or recirculation, or was causing metal damage to the pump (Figure 3).
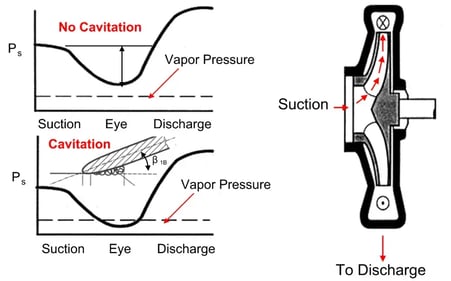
Figure 1: Damaging pump cavitation may occur when the static pressure in the fluid flow path falls below the liquid’s vapor pressure, causing bubbles to form. The bubbles violently collapse as the flow continues through the flow path encountering higher pressure. The collapsing bubbles may create localized shock waves against a component surface (impeller vane, piping, diffuser vane, casing, etc.). The typical root cause of cavitation is operating the pump with too low of a suction pressure.
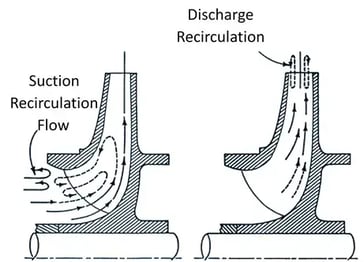
Figure 2: Damaging cavitation can also occur due to flow recirculation at the pump suction or discharge. Pressure in the recirculating flow falls below the liquid's vapor pressure, causing bubbles to form with the bubbles collapsing when encountering higher pressure. The collapsing bubbles may create localized shock waves against a component surface (impeller vane, piping, diffuser vane, casing, etc.). The root cause of recirculation is operating the pump too far away from its Best Efficiency Point (BEP).
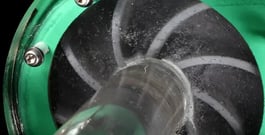
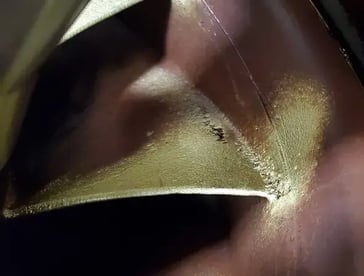
Figure 3: Top. Cavitation being observed through viewing ports during a test. Bottom. This is an example of pitting damage caused by cavitation.
What measurement methods were utilized?
MSI had the opportunity to measure pressure pulsations with: 1) dynamic pressure transducers, 2) sound pressure with microphones, and 3) external high-frequency (short time period or instantaneous) casing acceleration. At the time, sound pressure microphones or dynamic pressure transducers were considered the primary method for measuring damaging cavitation.
The new non-intrusive test method used high-frequency casing accelerometers temporarily mounted on the pump piping and casing (Figure 4) as an effective indicator of cavitation severity. Based on experience MSI now knows that measurements above approximately 100 g indicate conditions capable of causing metal-removal damage, while levels below approximately 30 g were associated with nuisance cavitation noise. At the time, a Modified Goodman Diagram was used to determine what amount of acceleration would cause metal removal damage for a given material.
What was the most effective method for determining if the cavitation was damaging?
The investigation determined that suction recirculation was occurring at flow rates above BEP. The oversized pump suction, selected to satisfy stringent NPSH requirements, contributed to an unstable flow pattern entering the pump. This instability produced cavitation surge, resulting in periodic chugging, vibration, and cavitation erosion.
An example of the measured data is shown in Figure 5. By measuring the instantaneous acceleration spikes, MSI can directly measure the pump’s material response to the cavitation events. Measuring the sound frequency spectrum provides a less direct measurement since the effects must be transmitted from the pump casing to the air before being measured, and gives ambiguous indications.
Even more difficult‐to‐perform dynamic pressure or hydrophone measurements are less direct because they provide no information about whether cavitation bubbles are harming the metal. MSI has since used the non-intrusive high-frequency accelerometer method in well over a hundred field troubleshooting projects.
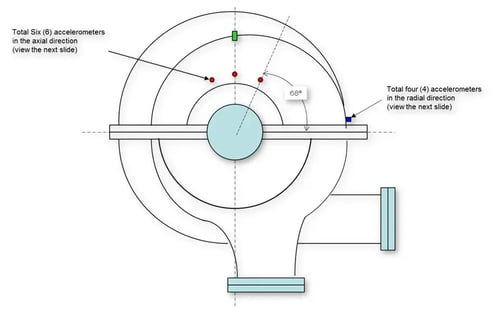
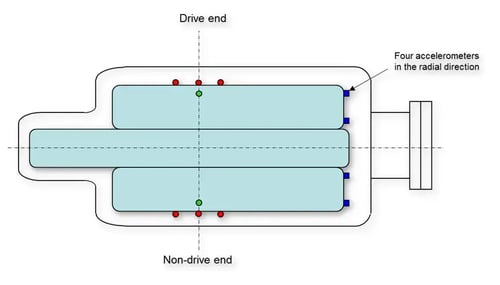
Figure 4: Locations for temporary use of high-frequency accelerometer measurements on the pump casing and nearby piping.
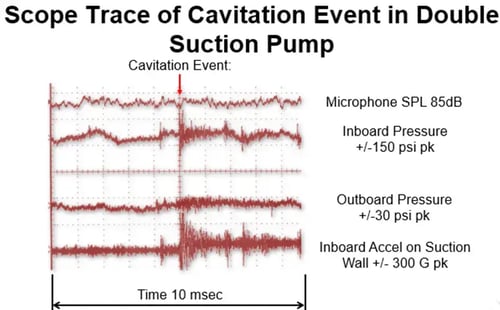
Figure 5:Scope trace of a cavitation event in a double suction pump comparing three measurement types. Top – Microphone was the least effective. Middle – More time-consuming intrusive dynamic pressure measurements showed the highest pressure fluctuations were on the inboard (driver) side of the double impeller – confirmed by a follow-on physical inspection. Bottom – Non intrusive high-frequency accelerometer measurements. Acceleration above 100G pk indicates that metal removal damage is taking place. If below 30G, the flow path design is such that the cavitation bubb are collapsing midstream in the flow path.
How was the pump problem solved?
The solution included:
- Modifying the impeller design
- Changing impeller materials
- Changing wear-ring materials
These modifications addressed the hydraulic conditions contributing to cavitation and improved component durability.
What were the results?
The pump cavitation assessment delivered significant reliability and cost improvements:
-
- Impeller life increased from less than 2 years to approximately 15 years
- Cavitation damage was identified and addressed
- Four duplicate pumps benefited from the solution
- Approximately $840,000 in repair costs were saved
What does this pump cavitation case history demonstrate?
Detecting cavitation is not enough; engineers must determine whether it is damaging the pump.
High-frequency vibration measurements, combined with operating data and engineering analysis, can help identify cavitation severity, determine root causes, and develop targeted solutions for pump cavitation, vibration, and premature component failure.
Frequently Asked Questions
What is pump cavitation?
Pump cavitation occurs when vapor bubbles form and collapse within a pump. Severe cavitation can cause noise, loss of performance, vibration, erosion, and premature component failure. There are several different types of cavitation.
What other flow Instabilities cause cavitation-like noise and damage?
Internal suction or discharge recirculation also leads to cavitation noise and possibly metal removal damage. It typically takes place at flow rates that are too low or too high relative to BEP.
How does the observed damage differ between cavitation and suction or discharge recirculation?
Cavitation pitting damage is observed on the suction side (low pressure) side of an impeller or diffuser blade during a physical inspection. This area is easily visible. Recirculation pitting is on the high-pressure or back side of an impeller vane. It may be difficult to see but the pitting can be felt by rubbing the high-pressure side of the vane during inspection.
How Does a Vibration Spectrum Differ Between Cavitation and Recirculation?
Cavitation increases the spectrum’s noise floor. Such broadband excitation is best observed in the time domain vibration plot. Recirculation is best observed in the more typical frequency domain spectrum with suction recirculation usually being at 65 to 95% of running speed and discharge recirculation at a 5 to 30% of running speed.
If the vibration spectrum indicates cavitation or recirculation, how do you determine if it is causing metal removal damage?
High-frequency vibration measurements, particularly instantaneous casing acceleration, can non-intrusively help determine whether cavitation is severe enough to cause material damage.
What is cavitation erosion?
Cavitation erosion is the gradual loss of material caused by repeated collapse of vapor bubbles against pump components such as impeller vanes, casing surfaces, and piping. The same type of damage can take place in other fluid components such as valves.
What were the results of this pump cavitation investigation?
The solution increased expected impeller life from less than two years to approximately 15 years and saved approximately $840,000 in repair costs across four pumps.